TLDR
Straight tuck end boxes are paperboard folding cartons with top and bottom tuck flaps that close from the same panel side. They are often useful as presentation-oriented product cartons, but the structure alone does not determine whether they can protect a product in ecommerce distribution. Specify the product fit, board, seam, closures, inserts, packing method, and outer shipping package as one system. Before approving artwork, confirm the dieline and dimension convention with the carton producer, then measure and record the final packed parcel separately.
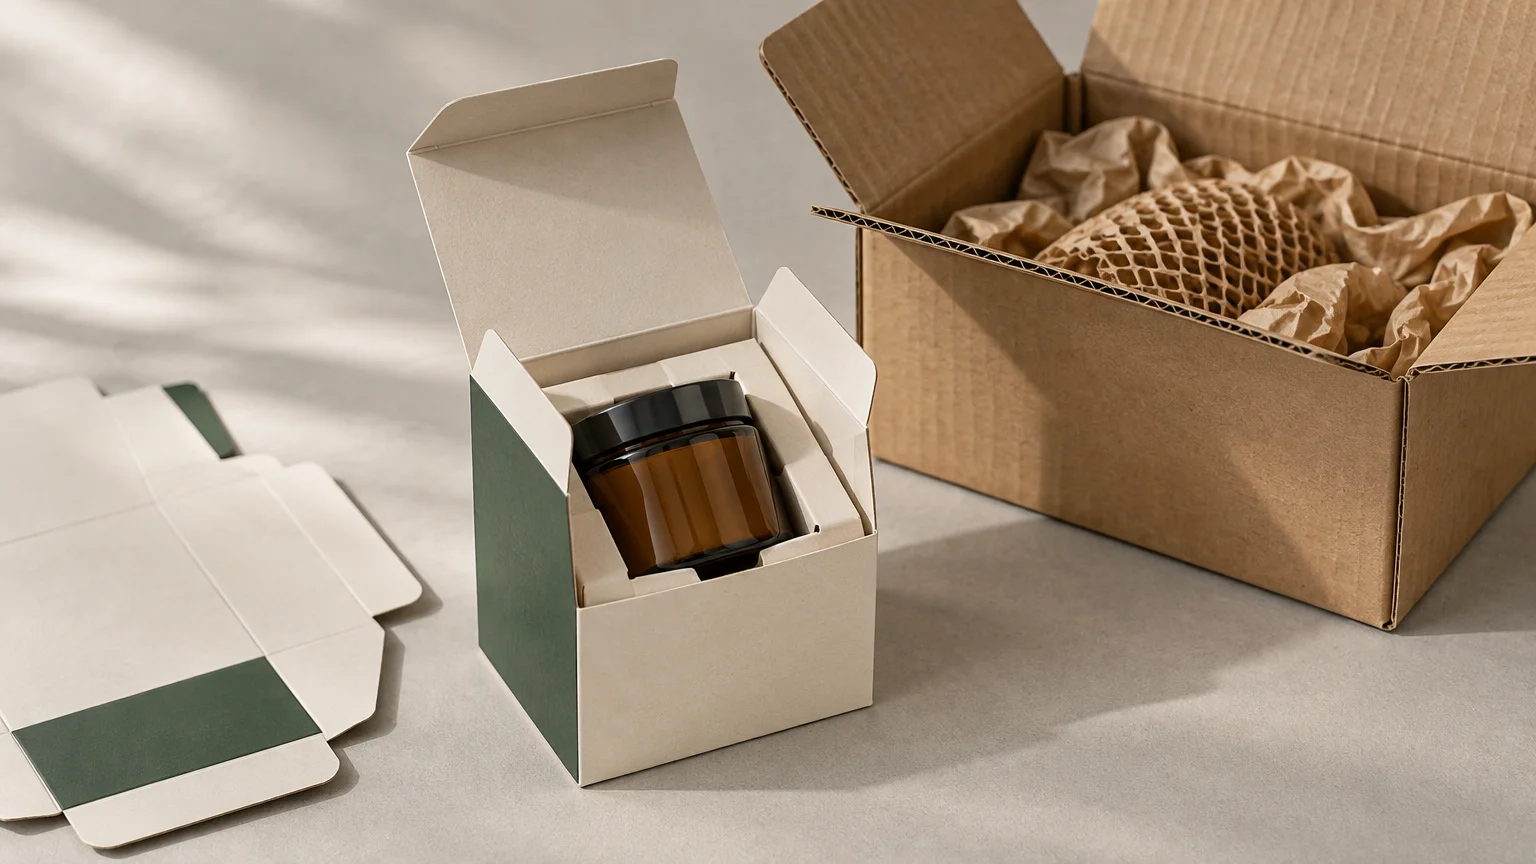
The practical reason to choose straight tuck end boxes is straightforward: they provide a clean, conventional folding-carton format that can be stored flat, assembled during packing, and printed as part of the customer-facing presentation. Both tuck closures fold from the same panel side, unlike a reverse tuck end carton, whose closures fold from opposite sides.
That definition is only the starting point. An STE carton may hold the product at retail, organize a kit, carry required information, or create a branded unboxing layer. It is not automatically a parcel-ready shipping box. Ecommerce operators must decide separately how the filled carton will survive storage, picking, packing, carrier handling, and delivery.
Where straight tuck end boxes fit
An STE carton is a practical candidate when the product needs a printable paperboard enclosure and its geometry, weight distribution, and closure requirements are compatible with a tuck-style structure. Common project categories can include small jars, bottles, tubes, personal-care products, accessories, electronics, and compact kits, but product category alone is not enough to establish suitability.
The complete pack-out matters more than the carton name. A relatively compact product can still create trouble if it has a high center of gravity, concentrated weight, fragile components, leaking risk, or enough movement to open or distort the carton. Conversely, a carefully fitted insert and a suitable outer shipper may make an STE carton work well as the presentation layer.
I would treat the selection as a sequence of operational questions:
- Does the carton need to serve as a retail or presentation package, an organizational sleeve for a kit, or the actual transport container?
- Can the carton support and retain the filled product without relying on artwork, coatings, or a label to solve a structural problem?
- Does the product require an insert, partition, tamper feature, seal, or secondary containment?
- Can packing staff form, load, close, and inspect it consistently at the expected order volume?
- Will the filled carton travel inside a corrugated mailer or shipping case, and what cushioning or void fill will that parcel need?
This system-level approach is also useful when planning broader custom ecommerce packaging. It prevents the branded carton from being selected in isolation from labels, protective materials, packing labor, and shipping requirements.
STE versus nearby carton options
| Structure | Defining characteristic | Operational reason to consider it | Question to resolve |
|---|---|---|---|
| Straight tuck end carton | Top and bottom tuck flaps close from the same panel side | A conventional presentation carton that can be supplied flat and formed during packing | Will the closure, seam, board, and any insert support the filled product? |
| Reverse tuck end carton | Top and bottom tuck flaps close from opposite panel sides | An alternative folding-carton layout that may suit a particular dieline, production plan, or packing orientation | Which panel orientation and loading sequence work best for the product and artwork? |
| Auto-lock-bottom carton | The bottom is designed to lock into position as the carton is formed | May reduce bottom-closing steps or provide a different base configuration | Does the added structural complexity improve the actual packing process and filled-product support? |
| Corrugated mailer or outer shipper | A fluted corrugated structure encloses the product or retail carton | Provides a separate transport layer that can accommodate protection and shipping labels | What board, fit, cushioning, and transit validation does the final parcel require? |
The distinction between STE and reverse tuck end concerns the direction of the closures. It does not, by itself, establish board strength, product protection, assembly speed, or shipping performance. Those outcomes depend on the full structural specification and pack-out.
An auto-lock bottom deserves consideration when the bottom-forming step is a recurring labor or support issue. It should not be selected merely because it sounds stronger or more automated. Ask the converter for representative samples and have the fulfillment team assemble them with the real product. A structural feature has value only if it improves the actual loading and closing sequence without introducing avoidable material, production, or inventory complexity.
Build a quote-ready carton specification
A request that contains only a product name and approximate box size transfers too many decisions to the supplier. A useful request for quotation should define the product, carton, production requirements, and shipping plan clearly enough for suppliers to identify assumptions.
Product and fit information
- Actual maximum product dimensions, including caps, pumps, protrusions, and manufacturing tolerance
- Filled product weight rather than an empty-container weight
- Product orientation and any relevant center-of-gravity or movement concern
- Clearance needed for loading, removal, protective wrapping, instructions, or accessories
- Whether an insert, partition, tray, or secondary containment component is required
- Any product-specific handling, regulatory, food-contact, moisture, or leakage requirement that the supplier must evaluate
Carton and production information
- Requested internal dimensions, subject to the supplier's confirmed dimension convention
- Straight tuck end structure and the intended loading orientation
- Board material and caliper proposed or approved for the filled product
- Side-seam construction and closure details
- Dieline identifier, artwork revision, print requirements, coatings, and finishing treatments
- Any seal, tamper-evident label, or closure-control requirement
- Order quantity, release schedule, packing configuration, delivery location, and storage constraints
Do not assume that every converter quotes dimensions in the same order or on the same internal-versus-external basis. Write the convention directly on the specification, ask the supplier to confirm it, and check a physical sample with the real product before production artwork is released.
If you are evaluating alternative printing options, send each supplier the same controlled specification and request that substitutions or assumptions be identified in writing. Otherwise, apparently comparable quotes may represent different board, finishes, packing formats, or structural interpretations.
Treat the retail carton and shipping parcel as separate configurations
The STE carton may be the package the customer sees first, but ecommerce shipping systems generally need information about the final parcel handed to the carrier. That parcel can include the product, STE carton, insert, protective material, corrugated outer shipper, void fill, documents, tape, and shipping label.
Shopify documentation states that saved package dimensions and weights are used in shipping workflows, while inaccurate information can contribute to shipping-label price adjustments. Shopify’s package setup guidance Record the outside dimensions and total weight of the final sealed shipment configuration rather than copying the folding carton's dimensions into the shipping system.
Carrier standards also change. USPS publishes parcel size and weight rules, including dimensional-weight information for applicable parcels, so current requirements and fees should be checked when the shipping configuration is approved. Avoid building a permanent packaging rule around an old threshold or surcharge table.
Transit evaluation should represent the package as shipped. ISTA materials distinguish between packaged products that travel in an over-box and products designed to ship in their own container, and its testing resources address distribution hazards. ISTA’s transit-testing information can help teams identify the appropriate evaluation path, but the exact protocol should match the product and distribution system.
A worked example: a glass jar in an STE carton
Consider a brand putting a filled glass jar into a printed STE carton. The team should begin with the jar's maximum physical dimensions, closure profile, filled weight, and tolerance—not a nominal volume or an early design rendering.
Next, determine whether the jar can sit directly in the carton or needs an insert to limit movement and protect vulnerable areas. The insert changes the required internal dimensions, assembly sequence, material count, and unit cost. If a seal or tamper feature is needed, define whether it belongs on the jar, the carton, or both; do not leave that decision to the artwork stage.
The supplier can then develop or confirm a dieline around the agreed internal fit, board, seam, tuck closures, and insert. The team should assemble samples using production-representative jars, confirm that the bottom and closures remain secure, and document how the carton is loaded.
Finally, place the approved retail carton into its proposed corrugated shipper with the planned protection. Seal it as fulfillment would, attach the label in the intended position, and measure the outside dimensions and total parcel weight. Those parcel measurements—not the jar size or STE dieline—belong in the applicable shipping configuration.
Control the carton as a SKU-level packaging component
Once approved, the carton needs the same operational control as any other inventory item. Assign a component SKU or unambiguous item code and connect it to the products, bundles, regions, or campaigns allowed to use it. Maintain a packaging bill of materials that identifies the carton, insert, seal, outer shipper, documents, and other required components.
The controlled record should include the dieline revision, artwork revision, supplier item reference, approved material, pack quantity, effective date, and disposition of obsolete stock. Photograph the approved assembled carton and final pack-out from useful angles. Store those images with concise work instructions at the packing station or in the warehouse system.
Version control becomes especially important when regulatory copy, product counts, ingredients, languages, barcodes, promotions, or seasonal graphics change. A routing process based on product SKU and release date can keep old and new cartons from being mixed; the same principle applies to seasonal packaging routing by SKU and ship date. If variable identification or sealing is added later, define whether it is a functional label or a branded sticker before changing the bill of materials. The distinction between labels and stickers affects purchasing and packing controls.
Quote-readiness checklist
- Measure a production-representative product and document dimensional tolerances.
- Provide the filled weight and describe orientation, movement, fragility, or leakage concerns.
- State whether requested carton dimensions are internal or external and confirm the dimension order.
- Identify the STE structure, seam, loading direction, closure details, board, and proposed caliper.
- Specify inserts, partitions, seals, tamper features, coatings, and finishing requirements.
- Provide quantities, release timing, delivery points, case-packing needs, and storage constraints.
- Separate the retail-carton specification from the final ecommerce parcel configuration.
- Approve a physical sample and production dieline before releasing final artwork.
- Document the assembled pack-out and record the final sealed parcel's outside dimensions and weight.
- Assign component SKUs and revision controls before cartons enter fulfillment inventory.
Make the structural decision before the artwork decision
Straight tuck end boxes fit ecommerce best when they are treated as one controlled component in a larger packaging system. Choose the structure around the real product and packing process, not around a flat artwork mockup. Then confirm the dieline, dimension convention, board, seam, closures, insert, and outer shipping configuration before committing to production.
The next useful step is to create one specification sheet and one production-representative sample pack-out. If the supplier, designer, purchasing team, and fulfillment lead can all use those same controlled references, the carton is far less likely to become a source of packing delays, obsolete inventory, or incorrect shipping data.